10 Industrial Applications of Silicone Rubber
Silicone rubber is one of the most versatile elastomer materials used in modern industry. Known for its heat resistance, electrical insulation, flexibility, weatherability and chemical stability, silicone rubber is widely selected for demanding applications where ordinary rubber materials may fail. From power transmission and cable systems to medical devices, EV components and food-contact parts, silicone rubber continues to play an important role in high-performance manufacturing.
In practical sourcing and engineering discussions, buyers often search for the right silicone rubber grade by application rather than by chemistry alone. A compound used for composite insulators is very different from one designed for medical tubing or food-grade seals. Understanding where silicone rubber is used helps manufacturers select the right hardness, curing system, thermal resistance and compliance profile for the final product.
This guide explains 10 industrial applications of silicone rubber and shows why the material remains a preferred option in electrical, transportation, healthcare and industrial processing environments.
Why Silicone Rubber Is Widely Used in Industry
Before looking at specific industries, it helps to understand why silicone rubber is so widely used. The material combines several properties that are difficult to achieve in one conventional elastomer. It can remain flexible across a broad temperature range, perform well under UV and weather exposure, provide excellent electrical insulation and resist moisture, ozone and many outdoor service conditions.
In industrial supply chains, silicone rubber is also valued for its processing versatility. It can be supplied as HTV or HCR compounds for extrusion, compression molding and transfer molding, or as liquid silicone rubber for injection molding. This makes it suitable for both large structural insulation parts and precision molded components.
| Key Property | Why It Matters in Industry |
|---|---|
| Heat Resistance | Helps components remain stable in high-temperature operating environments. |
| Cách điện | Supports safe use in power, cable, electronics and EV systems. |
| Khả năng chống chịu thời tiết | Improves long-term outdoor performance under UV, ozone and moisture exposure. |
| Độ đàn hồi | Allows sealing, vibration control and flexible component design. |
| Tính ổn định hóa học | Useful in harsh industrial and processing environments. |
| Processability | Can be extruded, molded or calendered into many industrial forms. |
1. Composite Insulators for Power Transmission
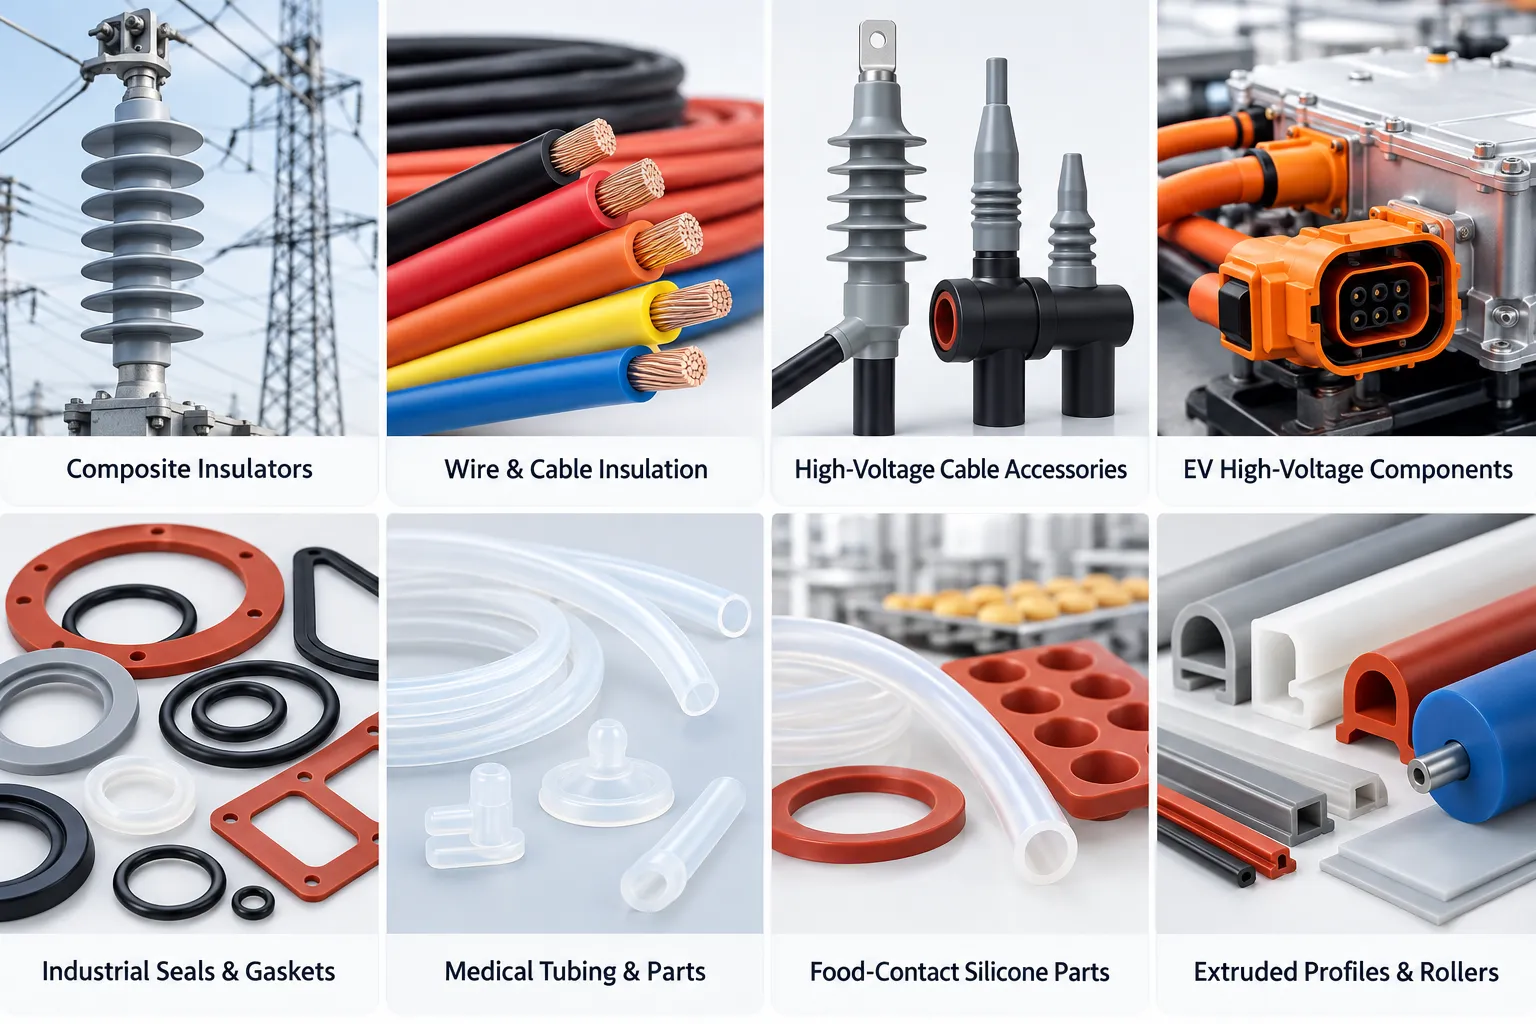
One of the most important industrial applications of silicone rubber is in composite insulators used in high-voltage transmission and distribution systems. In these products, silicone rubber is commonly used as the external housing or shed material because it provides hydrophobicity, weather resistance and electrical insulation. These characteristics help reduce leakage current and improve performance in polluted or humid service environments.
Compared with traditional ceramic materials, silicone rubber composite insulators are lighter in weight and easier to transport and install. They also perform well in outdoor service because the material surface can maintain or recover hydrophobicity, which is critical in contaminated operating conditions.
2. High-Voltage Cable Accessories
Silicone rubber is widely used in cable accessories such as cable terminations, joints, stress cones and insulation sleeves. In high-voltage cable systems, the material must provide reliable dielectric performance while also tolerating mechanical stress, outdoor conditions and elevated temperatures.
The combination of flexibility and electrical insulation makes silicone rubber especially useful for prefabricated cable accessories. It can be engineered to maintain dimensional stability and consistent insulating performance, which is essential in power infrastructure projects and industrial electrical systems.
3. Wire and Cable Insulation
In the wire and cable industry, silicone rubber is selected for applications that require high temperature resistance, flexibility and electrical insulation. It is often used in industrial cable, heating cable, appliance cable and specialized power cable systems. In demanding cable environments, conventional rubber may harden or degrade, whereas silicone rubber can maintain flexibility over a wider service temperature range.
Some cable grades are also formulated for flame resistance or low-smoke performance, making silicone rubber especially attractive in safety-sensitive applications where thermal stability and fire behavior matter.
4. EV and New Energy Vehicle Components
As electric vehicles continue to expand globally, silicone rubber has become increasingly important in EV high-voltage systems. It is used in connector seals, cable protection parts, grommets, boots, insulating components and thermal interface-related sealing parts. These applications require strong electrical insulation together with heat resistance and long-term reliability.
Silicone rubber is especially useful in EV design because battery systems and high-voltage assemblies operate under thermal stress and require safe insulation performance. The material can also be tailored for orange high-voltage component identification and flame-retardant performance where required.
5. Industrial Seals and Gaskets
Seals and gaskets are among the most common industrial applications of silicone rubber. The material is widely used in equipment sealing systems where temperature resistance, compression recovery and environmental durability are important. Silicone rubber gaskets can be found in industrial machinery, lighting systems, enclosures, pumps, processing equipment and outdoor control cabinets.
Its ability to remain flexible over time helps improve sealing reliability, especially in environments exposed to heat, weather or repeated assembly cycles. For many industrial OEMs, silicone rubber offers a practical balance between performance and manufacturability.
6. Medical and Healthcare Components
Silicone rubber is also used in healthcare and medical manufacturing. Depending on the compound type and compliance profile, it may be used in tubing, valves, soft molded parts, respiratory components, handles, seals and wearable-contact parts. Medical applications require more than basic material performance. Cleanliness, biocompatibility and process consistency are often just as important as flexibility and durability.
Not all industrial silicone rubber grades are suitable for healthcare use, but the broader medical market remains one of the most recognized application areas for specialized silicone materials.
7. Food Processing and Food-Contact Parts
In the food processing industry, silicone rubber is used for seals, tubing, molded parts, gaskets and other components that may come into contact with food or beverages. The material is favored because of its flexibility, heat resistance and ability to be formulated for food-contact compliance. In many cases, manufacturers need materials that can tolerate repeated cleaning cycles, changing temperatures and long service periods without losing sealing performance.
For export markets, food-grade silicone rubber compounds may also need to support regulatory requirements such as FDA 21 CFR, LFGB, REACH or BfR-related expectations, depending on the destination market.
8. Electronics and Electrical Insulation Parts
Silicone rubber is commonly found in electronic and electrical assemblies where insulation, soft protection and environmental resistance are required. Examples include keypad components, insulating boots, protective covers, cable entry parts and molded insulating barriers. Because the material can maintain electrical performance under a wide range of temperatures, it remains useful in both indoor electronics and outdoor electrical equipment.
Its resistance to UV and weathering also makes it attractive for lighting products, outdoor boxes and industrial controls exposed to harsh operating conditions.
9. Industrial Rollers, Sheets and Extruded Profiles
Beyond molded parts, silicone rubber is also manufactured into sheets, strips, tubes, cords and extruded profiles for industrial use. These forms are used in ovens, textile equipment, packaging machinery, conveyor-related systems, printing machinery and thermal process lines. Silicone rollers and silicone sheets are particularly useful where heat resistance and elastic surface performance are required.
Extruded silicone rubber products are also widely used for sealing strips, cable protection and thermal barriers in industrial assemblies. This makes silicone rubber not only a material for finished components, but also a structural industrial processing material.
10. Aerospace and Transportation Components
In aerospace and broader transportation systems, silicone rubber is used in sealing, insulation and protective applications. These sectors value the material for its stability under temperature variation, environmental exposure and mechanical cycling. Railway, bus, heavy equipment and aviation-related systems may all use silicone rubber in selected sealing or insulating positions.
The exact performance requirements vary, but the material’s durability and temperature tolerance continue to make it an important engineering option in transportation manufacturing.
Which Silicone Rubber Type Is Used in These Industries?
Different application sectors do not use exactly the same silicone rubber type. The choice depends on processing method, product structure and performance target. In general, HTV or HCR silicone rubber is widely used for cable, composite insulator, sealing and industrial molded applications. LSR is more common in precision injection-molded components and some medical or consumer applications. RTV silicone is often selected for on-site sealing, potting or coating-related use rather than bulk compound processing.
| Silicone Type | Typical Industrial Use |
|---|---|
| Cao su silicone HTV / HCR | Composite insulators, cable accessories, extruded profiles, seals, sheets and industrial molded parts |
| LSR | Precision molded components, medical parts, food-contact components and high-volume injection molding |
| Silicone RTV | Sealing, bonding, potting and field-applied insulation or protection systems |
How to Choose Silicone Rubber for an Industrial Application
Although silicone rubber is highly versatile, material selection should always begin with the real operating environment. Engineers and buyers should look at service temperature, required hardness, flame resistance, electrical properties, outdoor durability, processing method and any industry-specific compliance requirement. In practical sourcing, it is also important to decide whether the material will be molded, extruded, calendered or injection processed, because this directly affects compound selection.
For example, the ideal silicone rubber compound for a high-voltage composite insulator may need outstanding hydrophobicity and tracking resistance, while a food processing gasket may require food-contact compliance and clean molding performance. A cable material may prioritize flame resistance and extrusion stability, whereas an EV component may require thermal aging stability and dielectric reliability.
Common Questions Buyers Should Ask
What is the final application?
Material selection should begin with the actual end-use environment and part function.
What hardness is required?
Different products may need soft, medium or high-hardness silicone compounds.
Will the part face heat or flame?
Temperature resistance and flame-retardant requirements should be defined early.
Is electrical insulation critical?
Power, cable and EV applications often require controlled dielectric performance.
Will the product be used outdoors?
UV resistance, ozone resistance and weatherability become more important in outdoor service.
Are compliance documents needed?
Food, medical and export applications may require additional documentation or testing support.
Kết luận
Silicone rubber has become a strategic material across many industrial sectors because it combines heat resistance, flexibility, electrical insulation and weather durability in one elastomer system. Its industrial value is especially clear in power transmission, cable accessories, EV systems, industrial sealing, electronics, medical devices and food-contact manufacturing.
These 10 industrial applications of silicone rubber show that the material is not limited to one market. Instead, it serves as a cross-industry engineering solution that can be tailored to different performance requirements through formulation and processing. For manufacturers, buyers and product designers, understanding the target application is the first step toward choosing the right silicone rubber grade.