Silicone Rubber Injection Molding for Composite Insulators
Silicone rubber is one of the most important housing materials used in modern composite insulators. Its hydrophobicity, weather resistance, electrical insulation and resistance to tracking and erosion make it highly suitable for transmission lines, distribution systems, substations and other outdoor high-voltage applications.
But material performance alone is not enough. To produce a reliable composite insulator, the silicone rubber must be molded consistently around the fiberglass-reinforced polymer core, form the sheds accurately, bond properly to the internal structure and cure without voids, incomplete filling or surface defects.
Injection molding is widely used for this purpose because it can form complex shed geometries with good repeatability and production efficiency. This article explains how silicone rubber injection molding for composite insulators works, which material properties matter, what can go wrong during production and how manufacturers can improve molding consistency.
Why Silicone Rubber Is Used for Composite Insulator Housings
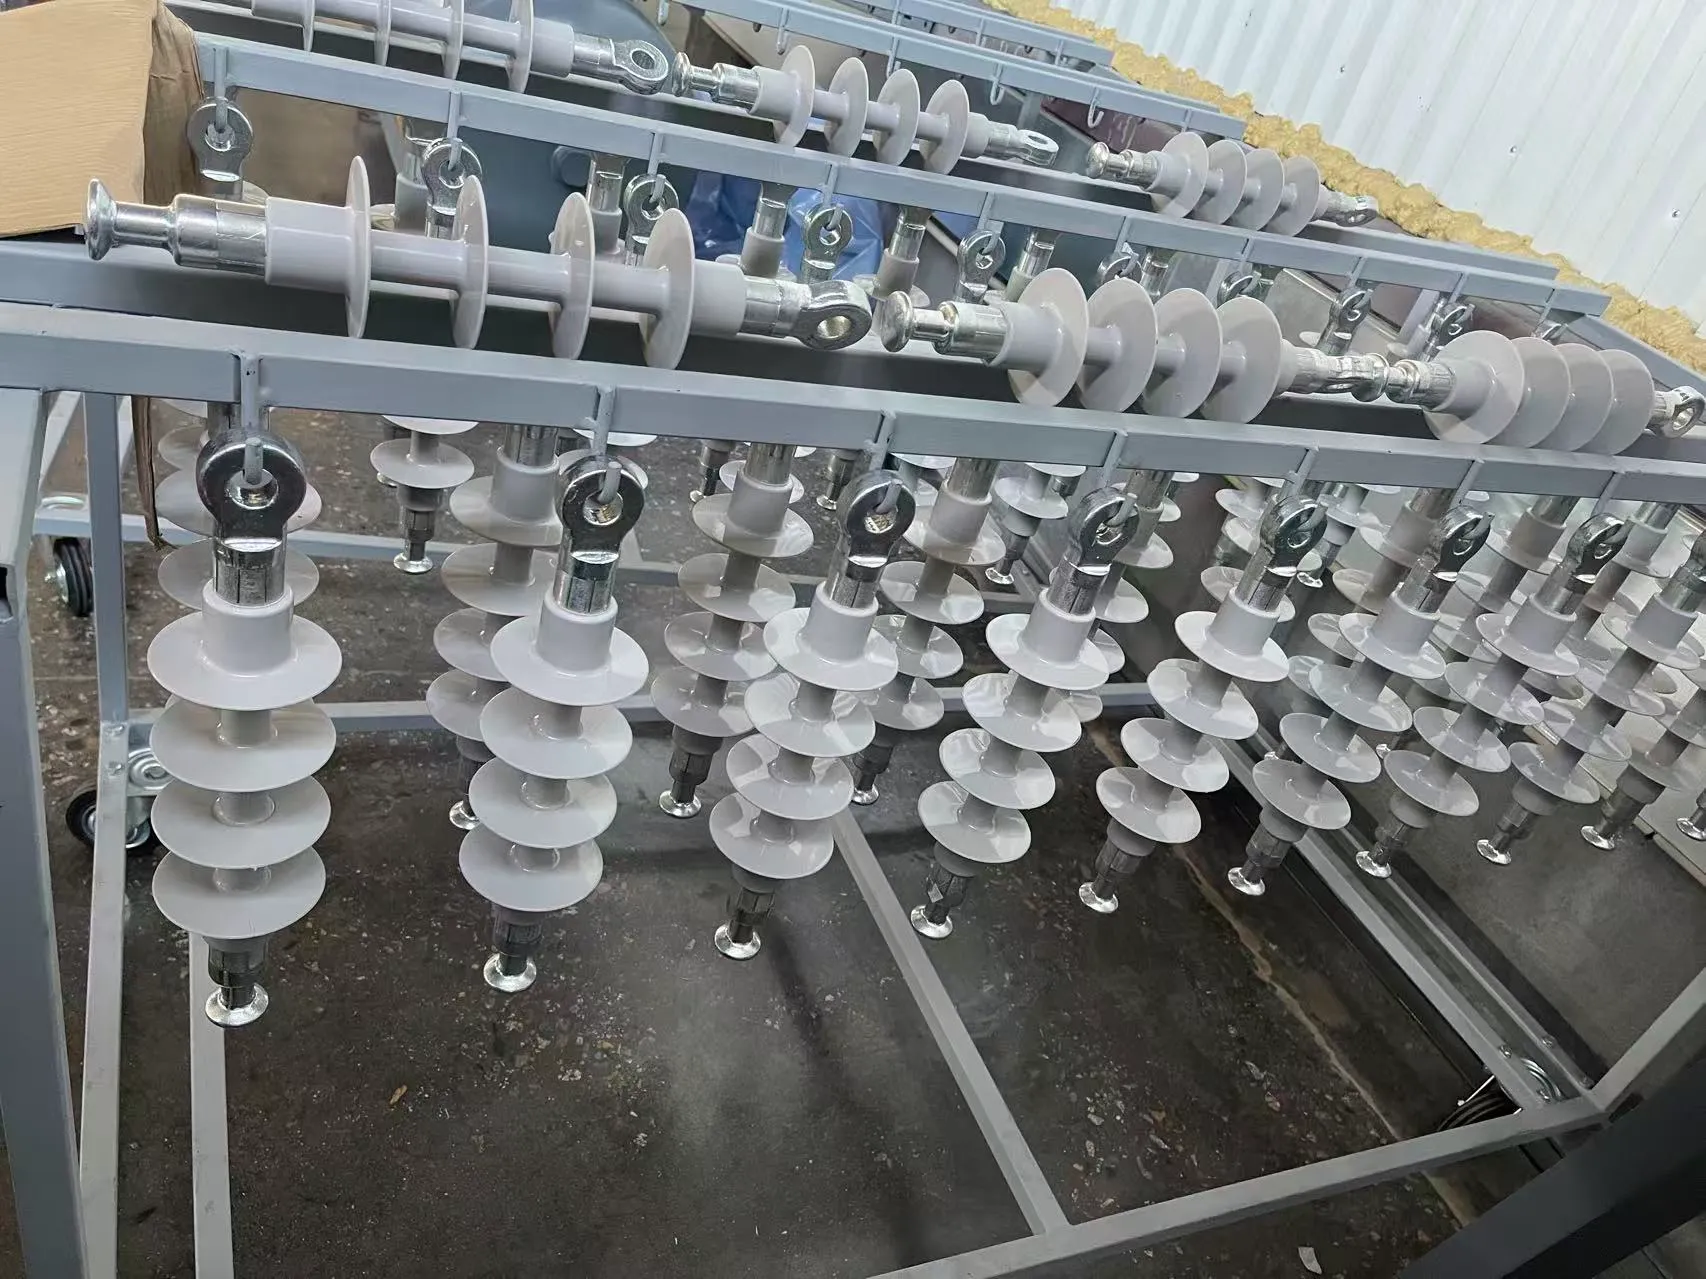
A composite insulator is typically made from several functional components rather than a single material. The internal FRP rod provides the main mechanical strength, metal end fittings connect the insulator to the power system, and the silicone rubber housing provides the external insulating surface and sheds.
The housing must operate outdoors for years while exposed to electrical stress, rain, fog, contamination, sunlight, ozone, heat and repeated temperature changes.
These properties explain why silicone rubber is widely selected for composite insulator housings, but they must survive the molding process and remain consistent in the finished product.
What Type of Silicone Rubber Is Used for Composite Insulators?
Composite insulator manufacturers commonly use specialized electrical-grade HTV/HCR silicone rubber rather than a general-purpose silicone compound.
HCR, or high consistency rubber, is a solid or gum-like silicone material. HTV refers to high-temperature vulcanizing silicone rubber. In industrial electrical applications, the two terms frequently overlap because high-consistency silicone compounds are normally cured using heat.
The formulation may contain silicone gum, reinforcing silica, ATH or other mineral fillers, processing aids, pigments and a curing system.
The final compound must provide a balance between electrical performance, mechanical strength and processability.
Why Injection Molding Is Used for Composite Insulators
Composite insulator housings contain repeated sheds and relatively complex geometries. The silicone rubber needs to fill the mold around the FRP core and form thin shed sections without leaving voids or incomplete areas.
Injection molding can provide several production advantages when the material, tooling and process conditions are properly matched.
| Injection Molding Advantage | Pourquoi est-ce important ? |
|---|---|
| Repeatable Mold Filling | Helps produce consistent shed geometry across production batches. |
| Complex Shapes | Allows silicone to fill housing profiles and multiple shed sections. |
| Efficacité de la production | Can support shorter and more repeatable molding cycles than manual methods. |
| Controlled Material Flow | Helps manage how the compound moves around the core and through thin sections. |
| Consistent Cure | Controlled mold temperature and cycle conditions support repeatable vulcanization. |
However, injection molding also creates greater demands on compound rheology. A silicone rubber that performs well in compression molding may not necessarily provide the same behavior in an injection process.
How Silicone Rubber Injection Molding Works
The exact manufacturing sequence varies by insulator design and equipment, but the general process follows several core stages.
Prepare the FRP Core and End Structure
The fiberglass-reinforced rod and end fittings are prepared according to the insulator design. Surface condition and cleanliness are important because contamination can affect bonding and interface reliability.
Prepare the Silicone Rubber Compound
The HTV/HCR silicone compound must have consistent plasticity, dispersion and curing behavior. Depending on the material supply format, the cure system may already be incorporated or may require controlled preparation before molding.
Load the Core into the Mold
The prepared FRP core is positioned accurately inside the mold. Alignment is important because uneven positioning can create inconsistent housing thickness or shed geometry.
Inject the Silicone Rubber
The silicone compound is forced into the heated mold under controlled pressure. It must flow around the core and fill the shed cavities before significant curing prevents further movement.
Vent Air from the Mold
Air trapped inside the mold needs a controlled path to escape. Poor venting can produce voids, burn marks, incomplete filling and weak surface regions.
Vulcanize the Silicone Housing
The heated mold initiates curing and forms the crosslinked silicone rubber network. Cure time and mold temperature must be appropriate for the compound and part geometry.
Open the Mold and Demold
After sufficient curing, the insulator is removed carefully. Thin shed edges can be damaged if tear strength is too low or if the demolding force is excessive.
Inspect the Finished Housing
The molded insulator is checked for flash, incomplete filling, tears, voids, surface contamination, interface defects and dimensional consistency.
Silicone Rubber Flow Is Critical During Injection Molding
One of the most important material characteristics in composite insulator injection molding is how the uncured silicone rubber flows under pressure and temperature.
If the compound is too resistant to flow, it may not completely fill thin shed cavities or long flow paths before curing begins. Excessive pressure may then be required, increasing stress on tooling and the internal structure.
If the compound flows too easily, other problems may occur, including excessive flash or poor control around parting lines.
The goal is not simply to make the silicone softer. The formulation must provide the correct rheological behavior for the molding system.
Why Shore A Hardness Does Not Predict Mold Flow
A common misconception is that lower-hardness silicone rubber will automatically flow more easily during injection molding.
Shore A hardness is measured after the silicone has cured. Injection behavior depends mainly on the uncured compound's rheology, including polymer molecular weight, filler system, plasticity and processing aids.
Two compounds can both cure to 60 Shore A while requiring very different injection pressures or showing different mold-filling behavior.
| Propriété | What It Tells You |
|---|---|
| Shore A Hardness | Firmness of the cured silicone rubber |
| Plasticité | Behavior of the uncured high-consistency compound |
| Rheology | How the material deforms and flows under processing conditions |
| Cure Characteristics | How quickly the compound begins and completes vulcanization |
Why ATH Content Matters
Electrical-grade silicone rubber for composite insulators commonly uses ATH, or aluminum trihydrate, as part of the filler system.
ATH can support tracking and erosion resistance under severe electrical stress. This is important because outdoor insulators may experience leakage current, dry-band arcing and localized heating under contaminated and wet conditions.
However, increasing mineral filler content changes the processing behavior of the silicone compound.
The compound therefore needs a carefully balanced polymer, filler and processing-aid system rather than simply the highest possible ATH loading.
Reinforcing Silica and Mechanical Strength
Reinforcing silica is another important component in silicone rubber formulation. It helps develop tensile strength, tear strength and other mechanical properties.
The silica system also affects the uncured compound. Surface area, treatment, filler loading and dispersion can influence viscosity and molding behavior.
Poor dispersion can create weak areas or inconsistent processing, while excessive reinforcement may make mold filling more difficult.
The formulation needs enough mechanical reinforcement to protect the sheds without creating an unnecessarily difficult injection process.
Tear Strength Is Especially Important During Demolding
The sheds of a composite insulator are relatively thin compared with the central housing. During demolding, these sections may flex significantly as the finished insulator is removed from the mold.
If the silicone rubber has insufficient tear resistance, a small edge defect can develop into a larger tear.
| Possible Cause of Shed Tearing | What to Check |
|---|---|
| Low Tear Strength | Compound mechanical properties and formulation |
| Incomplete Cure | Mold temperature, cure time and compound cure characteristics |
| Sharp Mold Features | Mold design and edge radius |
| Excessive Demolding Force | Removal method and mold surface |
| Thin Shed Geometry | Design thickness and local stress concentration |
High tear strength silicone rubber can improve resistance to damage, but it should be combined with appropriate mold design and cure control.
Bonding Between Silicone Rubber and the FRP Core
The interface between the silicone housing and the fiberglass core is critical to composite insulator reliability.
If the interface contains contamination, weak bonding or voids, moisture may eventually penetrate into the internal structure. This can undermine insulation performance and expose the FRP rod to environmental attack.
Surface preparation, primer or bonding systems where applicable, mold conditions and material compatibility all influence interface quality.
Why Venting Is Important in Silicone Rubber Injection Molding
Air occupies the mold cavity before silicone rubber enters. As the compound fills the cavity, that air must escape.
If venting is insufficient, air can become trapped in thin shed regions, around the core or near the end of a flow path.
This may cause visible or internal defects.
Injection Pressure Must Be Controlled
Injection pressure must be high enough to move the high-consistency silicone compound through the runner system and into the complete housing geometry.
However, using excessive pressure to compensate for poor material flow or poor tooling is not an ideal solution.
Very high pressure can increase flash, stress the mold, contribute to core movement and make dimensional control more difficult.
The correct pressure therefore depends on the compound rheology, mold design, runner dimensions, insulator length and injection equipment.
There is no single injection pressure that is correct for every composite insulator.
Mold Temperature and Cure Time
HTV silicone rubber requires heat to vulcanize. During injection molding, mold temperature and cure time determine how quickly the material begins to crosslink and when the housing becomes strong enough for demolding.
If curing begins too early, the silicone may lose flow before the mold is completely filled. If curing is insufficient, the sheds may deform or tear during removal.
The correct cure window must be developed around the specific compound, mold geometry and equipment.
Common Injection Molding Defects in Composite Insulators
| Défaut | Possible Causes | Areas to Investigate |
|---|---|---|
| Incomplete Shed | Poor flow, early cure, insufficient pressure or trapped air | Compound rheology, mold temperature, injection settings and venting |
| Excessive Flash | Excess pressure, mold wear or excessive material flow | Clamping, mold condition and injection parameters |
| Air Voids | Poor venting or trapped gas | Vent design, injection sequence and mold filling |
| Torn Sheds | Low tear strength, under-cure or difficult demolding | Material, mold design and cure conditions |
| Surface Roughness | Poor compound flow, mold contamination or processing variation | Material consistency, mold surface and molding conditions |
| Poor Bonding | Surface contamination, interface preparation or compatibility problems | Core preparation, bonding process and compound compatibility |
| Dimensional Variation | Core movement, inconsistent fill or curing variation | Core positioning, material consistency and process controls |
Why Batch Consistency Matters
Composite insulator injection molding can be sensitive to changes in silicone rubber processing behavior.
If one material batch has different plasticity, filler dispersion or cure characteristics, the molding line may require changes in pressure, temperature or cycle time.
This can cause production instability even when the Shore A hardness remains within specification.
For high-volume insulator production, batch-to-batch consistency can be as important as achieving excellent laboratory properties in a single sample.
Electrical Properties Required After Molding
Injection molding must not compromise the electrical properties required from the finished silicone rubber housing.
Important characteristics may include dielectric strength, volume resistivity, hydrophobicity and resistance to tracking and erosion.
| Electrical Property | Importance for Composite Insulators |
|---|---|
| Rigidité diélectrique | Helps resist electrical breakdown through the silicone material. |
| Résistivité volumique | Helps limit current flow through the bulk housing material. |
| Hydrophobicité | Helps reduce continuous water-film formation under wet conditions. |
| Suivi de la résistance | Helps resist conductive path formation on contaminated surfaces. |
| Résistance à l'érosion | Helps resist material loss caused by electrical discharges and localized heating. |
These properties depend on the formulation as well as curing and manufacturing consistency.
Hydrophobicity After Injection Molding
Hydrophobicity is one of the defining advantages of silicone rubber composite insulators.
A hydrophobic surface causes water to form droplets rather than immediately spreading into a continuous conductive film.
This behavior helps reduce leakage-current development on contaminated surfaces under rain, fog or condensation.
The formulation must provide useful hydrophobicity while also maintaining the filler levels, mechanical strength and processing behavior required for injection molding.
Injection Molding vs Compression Molding for Composite Insulators
Both injection molding and compression molding can be used for silicone rubber components, but their processing characteristics differ.
| Comparison | Moulage par injection | Moulage par compression |
|---|---|---|
| Material Introduction | Compound is injected into a closed mold | Preformed material is placed directly into the mold |
| Mold Filling | Controlled flow through runners and cavities | Material spreads under mold closure and pressure |
| Automation Potential | Generally higher | Depends on production system |
| Complex Shed Geometry | Can provide strong repeatability when flow is optimized | Can also produce complex parts but material placement is different |
| Rheology Sensitivity | Very important | Important but different flow behavior |
| Efficacité de la production | Attractive for repeat production | Can be practical for selected designs and production volumes |
The preferred method depends on insulator size, tooling, available equipment, production volume and the silicone compound.
Long-Rod Composite Insulators Create Additional Challenges
Long transmission-line insulators can create longer flow paths and larger molding areas than small electrical components.
As the flow distance increases, maintaining consistent pressure, temperature and material behavior becomes more important.
Manufacturers may need to optimize gate locations, molding sequence, injection position and process control to ensure consistent filling along the entire housing.
Material variation that is barely noticeable in a small molded part may become much more obvious in a long composite insulator.
What Silicone Rubber Properties Should Manufacturers Specify?
A composite insulator compound should be specified around both processing and finished-product performance.
How to Evaluate a New Silicone Rubber Compound
Replacing an existing composite insulator silicone should not be based only on matching Shore A hardness or one electrical property.
A useful evaluation process should include laboratory testing and actual molding trials.
Why a Production Trial Is Essential
Two silicone rubber grades can have similar laboratory properties but behave differently on an injection molding line.
Differences in polymer structure, ATH content, reinforcing silica, processing aids and curing chemistry can affect injection pressure, mold filling and demolding.
A controlled production trial allows manufacturers to identify these differences before making a full material change.
During the trial, useful information includes actual injection pressure, filling time, cycle time, flash level, demolding behavior, surface appearance and defect rate.
How to Troubleshoot Incomplete Mold Filling
Incomplete mold filling is one of the most important injection molding problems because it directly affects shed geometry and housing integrity.
Possible causes include unsuitable compound rheology, low injection pressure, poor venting, early vulcanization, low material temperature, runner restrictions or excessive flow distance.
The solution should not automatically be to increase pressure.
How to Reduce Excessive Flash
Flash forms when silicone rubber flows into gaps along mold parting lines or other interfaces.
Potential causes include excessive injection pressure, poor mold closure, tooling wear or compound flow behavior that does not match the process.
Reducing flash may involve optimizing injection pressure, clamping force, compound rheology and mold maintenance.
Simply changing to a harder silicone rubber after curing does not necessarily solve the problem because cured hardness and uncured flow are different properties.
How to Reduce Shed Tearing
If shed tearing occurs repeatedly, manufacturers should investigate both the material and the molding process.
A higher-tear silicone grade may help when the current compound cannot tolerate the deformation required during demolding.
However, under-curing, sharp mold edges and excessive pulling forces can cause tearing even with a strong compound.
Quality Control After Injection Molding
Finished composite insulators should be inspected for both visible manufacturing defects and required material performance.
| Inspection Area | Typical Checks |
|---|---|
| Visual Housing | Incomplete fill, flash, contamination, burns, tears and surface defects |
| Shed Geometry | Diameter, spacing, profile and consistency |
| Core Interface | Bonding quality, voids and visible separation |
| Mechanical Properties | Hardness, tensile strength, elongation and tear strength as required |
| Electrical Properties | Dielectric and surface electrical performance according to specification |
| Traceability | Material batch, molding conditions and production lot |
What Should Be Included in a Silicone Rubber RFQ?
When sourcing silicone rubber for composite insulator injection molding, provide enough information for the supplier to understand both the electrical requirements and the actual production process.
Silicone Rubber for Composite Insulator Injection Molding from Yakows
Yakows supplies HTV/HCR silicone rubber compounds for composite insulator housings and other high-voltage electrical applications.
For injection-molded insulator applications, material selection can be evaluated around mold flow, plasticity, tear strength, tensile strength, elongation, hydrophobicity, dielectric performance, tracking and erosion resistance and batch-to-batch processing consistency.
Manufacturers replacing an existing compound can provide their current material properties together with actual production information such as injection behavior, mold filling, flash, demolding, shed tearing or incomplete filling.
The objective is not simply to match a datasheet. It is to identify a silicone rubber compound that can mold consistently around the FRP core while maintaining the electrical and environmental properties required throughout long-term outdoor service.
Foire aux questions
What silicone rubber is used for composite insulators?
Composite insulators commonly use specialized electrical-grade HTV/HCR silicone rubber formulated for hydrophobicity, tracking and erosion resistance, mechanical strength, outdoor aging and reliable molding.
Can silicone rubber be injection molded?
Yes. High-consistency silicone rubber can be processed using suitable injection molding systems, including applications such as composite insulator housings.
Why is silicone rubber injection molded around the FRP core?
The silicone housing forms the external insulating surface, sheds and environmental protection around the load-bearing fiberglass core.
Why does silicone rubber fail to fill the insulator mold completely?
Possible reasons include unsuitable rheology, insufficient injection pressure, poor venting, early curing, runner restrictions or excessive flow distance.
Does lower Shore A silicone flow better?
Not necessarily. Shore A measures cured hardness, while mold flow is determined by the rheology of the uncured silicone compound.
Why do composite insulator sheds tear during demolding?
Possible causes include insufficient tear strength, incomplete curing, sharp mold features, thin shed geometry or excessive removal force.
Why is ATH used in composite insulator silicone rubber?
ATH is commonly used in electrical silicone formulations to support tracking and erosion resistance under severe surface electrical stress.
What properties should be checked when changing silicone suppliers?
Manufacturers should compare mechanical, electrical and aging properties together with plasticity, cure characteristics, injection pressure, mold filling and demolding behavior.
Is injection molding better than compression molding?
Neither method is universally better. Injection molding offers strong automation and repeatability, while compression molding may be suitable for other production designs and equipment. The correct choice depends on the insulator, tooling and production requirements.
Why is a production trial important?
A production trial shows how the actual silicone rubber behaves in the real mold and injection system, which cannot be predicted from Shore A hardness or laboratory data alone.